
PCB SET Delivery and Panelization: Quantities and Acceptance
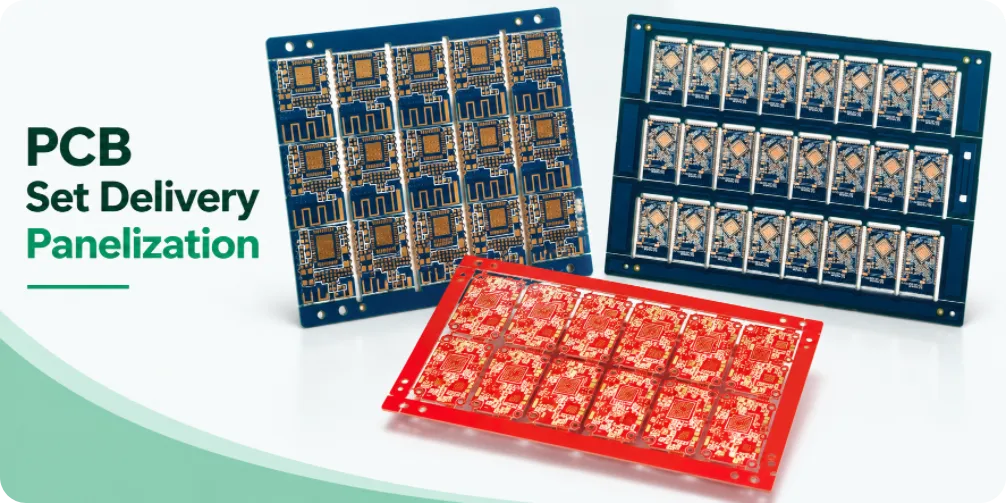
A purchase order for “500 SET” looks straightforward until one party interprets SET as a PCB panel and another means a kit of several different boards. That difference can cause quantity disputes even when every supplied PCB meets its drawing.
This PCB SET delivery and panelization guide addresses the purchasing side of the problem: identify what counts as a delivered unit, calculate exact panel quantities and specify how missing or rejected positions affect acceptance.
The examples distinguish individual circuits, complete arrays and multi-part kits. For the manufacturing-side basics, see the PCB panelization overview. The suggested PO clauses are examples to adapt, not replacements for negotiated order terms.
Table of contents
PCB PANEL AND DELIVERY QUANTITY
Need a Quote with Clear Delivery Units?
Share your panel drawing, circuits per array, required accepted quantity, packaging format and purchase-order requirements.
Request a PCB Quote →Define PCS, Array, Panel and SET Before Quoting
Four terms should be separated explicitly:
- PCS or piece: One finished PCB circuit of a stated design and revision, unless the purchase order expressly defines a different item.
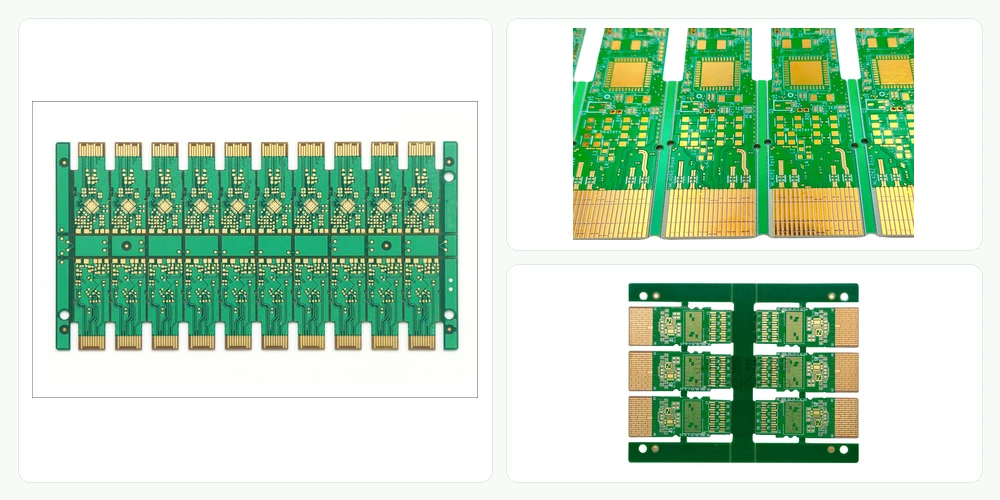
- Assembly array: A specified joined group of one or more PCB circuits, usually drawn with rails, breakaways and orientation information.
- Fabrication working panel: A manufacturing workpiece used inside the PCB factory; it may contain more than one assembly array. It is generally not a purchasing unit unless the contract says otherwise.
- SET or kit: A commercial unit whose contents must be defined. One SET may be one 12-up array of identical boards, or two A boards plus one B board, or some other contract-defined group.
The word panel is especially ambiguous. It can mean a large fabrication working panel or a smaller board array delivered to the customer’s assembly line. Purchase orders should name the intended drawing and unit instead of using an unexplained “panel count.”
| What the PO says | Why it is ambiguous | Better wording |
|---|---|---|
| “1,000 PCB” | Unknown whether loose singles or joined boards are expected | “1,000 accepted individual circuits, delivery format per PNL-01 Rev B” |
| “100 panels” | Number of good positions per panel not stated | “100 complete 12-up assembly arrays, each to PNL-01 Rev B” |
| “500 SET” | Contents of each SET unknown | “500 kits; 1 SET = 2 × PCB-A Rev C + 1 × PCB-B Rev D” |
| “Reject boards allowed” | Does not say how many, how marked or how counted | “Rejected positions prohibited in shipped arrays unless buyer approves a deviation” |
Calculate Delivered Quantities: Three Purchase Order Examples
Suppose an approved array drawing defines 4 columns × 3 rows = 12 identical circuits per array. The customer orders 1,200 accepted PCB pieces and agrees to receive them in complete, all-good 12-up arrays.
- Required complete arrays = 1,200 ÷ 12 = 100 arrays.
- Accepted pieces = 100 arrays × 12 accepted positions = 1,200 pieces.
- Packing list should state both 100 arrays and 1,200 accepted PCB pieces, together with the board and array revisions.
The arithmetic is simple only because every position in every shipped array must pass acceptance. If a supplier ships 100 physical arrays but one array includes one nonfunctional or omitted circuit, the shipment contains fewer than 1,200 accepted pieces. The contract should not automatically count an X-marked position as a shipped accepted board.
Example 2: Quantity Does Not Divide Into Complete Arrays
The same 12-up array is requested, but the buyer orders 1,000 accepted pieces.
- 83 complete arrays contain 83 × 12 = 996 pieces.
- 84 complete arrays contain 84 × 12 = 1,008 pieces.
- No integer number of complete all-good 12-up arrays contains exactly 1,000 pieces.
A practical purchasing process must now resolve the rounding or delivery policy before the supplier quotes or starts fabrication. Possible outcomes include an approved 1,008-piece over-delivery; delivery of 996 arrays plus four acceptable loose pieces; a separately approved partial array; or a revision of the ordered quantity. These are commercial alternatives, not permissions the shop can assume. Each option can affect price, packaging, testing, inventory receiving and batch traceability.
Why rounding up alone is not enough
If the PO demands 1,000 accepted pieces with no quantity tolerance, shipping 1,008 without approval can be a contract discrepancy. If a receiving system expects 84 panels, it may incorrectly book 1,008 pieces even when one position is marked as rejected. Therefore define the ordered unit, permitted over/under shipment, acceptable panel integrity and counting method in one place.
Example 3: A SET Contains Different Part Numbers
A chassis kit requires two PCB-A boards and one PCB-B board. The buyer writes 1 SET = 2 × A + 1 × B, and orders 480 complete SETs.
- A requirement: 480 × 2 = 960 accepted A pieces.
- B requirement: 480 × 1 = 480 accepted B pieces.
- Suppose A is delivered as complete 12-up arrays: 960 ÷ 12 = 80 all-good A arrays.
- Suppose B is delivered as complete 8-up arrays: 480 ÷ 8 = 60 all-good B arrays.
The supplier may deliver 80 A arrays and 60 B arrays, with packing and quantity records that permit assembly of 480 sets. There is no requirement to fabricate A and B on a combined mixed-design panel unless the customer deliberately releases such an array. Fabrication compatibility, assembly scheduling and revision control may make separate arrays preferable.
Kit completion is a different yield problem
If A arrives short but B is complete, the number of complete kits is limited by A’s available count. For instance, 958 acceptable A pieces and 480 B pieces can support only 479 complete kits with two A per kit, leaving some B inventory unused for kit completion. This illustrates why buyers should request good-piece counts by part number, not only panel counts or a combined carton quantity.
Agree How Rejected Positions Affect Acceptance
Some PCB operations identify bad circuits inside a multipiece panel. Such identification may be useful for downstream processing if the customer, assembler and test equipment support it. But whether an array with a rejected position is acceptable depends on the purchase specification. Do not treat bad-position marking as universally permitted—or universally forbidden.
Define the following policies in writing:
- All-good arrays versus mixed-status arrays. Must all positions pass, or can a rejected position remain in a shipped physical array?
- Counting convention. Are only passed positions included in billable delivered quantities?
- Identification. What accepted marking, map file, ID or electronic record identifies nonconforming positions?
- Replacement and shortage resolution. Who supplies replacement pieces, and in what delivery form?
- Traceability. Is lot identification tracked at the working-panel, array or individual-circuit level?
- Customer assembly compatibility. Can placement, AOI and test programs safely skip rejected positions without corrupting the manufacturing record?
For high-volume arrays, those rules also affect the cost model. The related volume-production panelization article explains why an all-good-array requirement changes the denominator in yield comparisons.
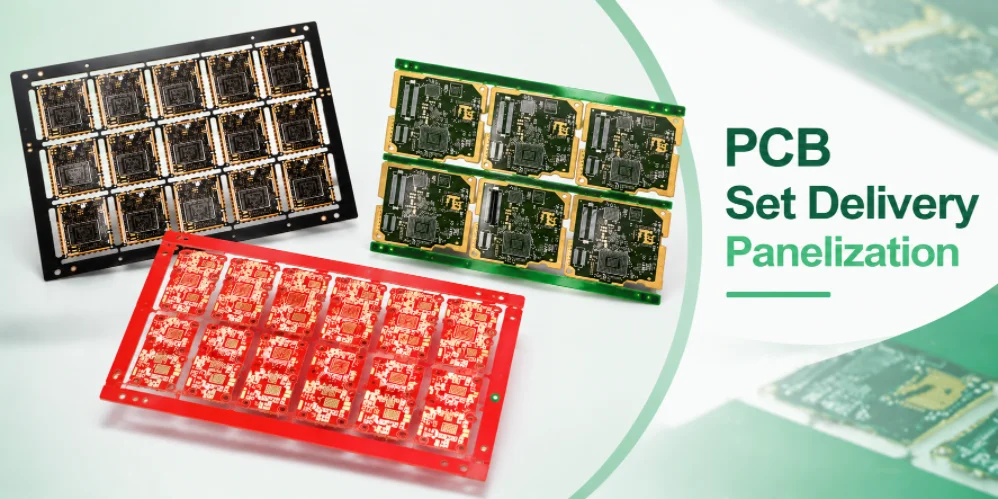
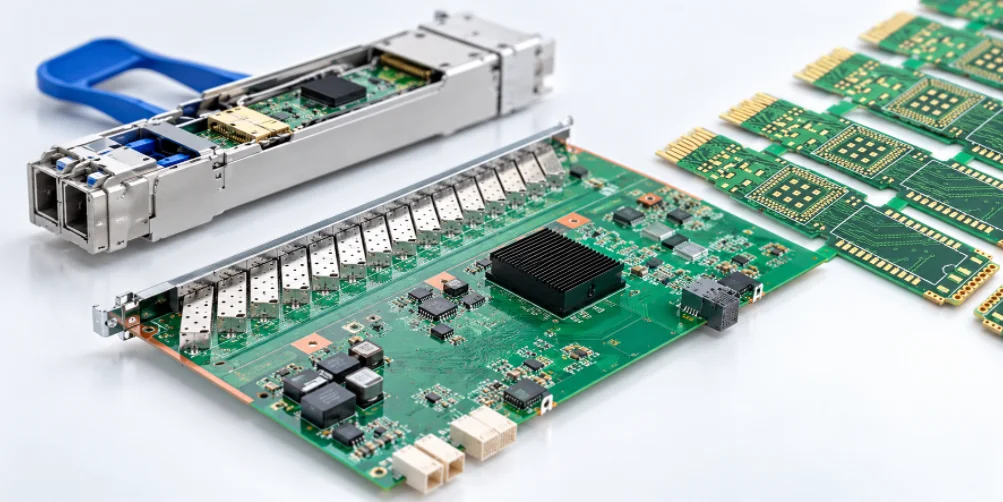
Populated and bare PCB arrays illustrating SET delivery formats
Choose the Delivery and Packaging Format
Joined arrays can be efficient when an SMT line expects rails, global fiducials or a particular conveyor orientation. But a customer may instead need individual boards for assembly fixtures, repair, warehousing or incoming inspection. A contract should identify the exact point at which the boards are separated and who is responsible for the resulting edge condition.
| Item to specify | Joined panel delivery | Individual-piece delivery |
|---|---|---|
| Quantity | Number of arrays and accepted circuits per array | Good pieces by part number and revision |
| Mechanical state | Rails and approved tabs/scores retained as required | Finished edges after controlled depaneling |
| Identification | Array-level ID plus bad-position policy | Piece/lot ID or carton batch identity |
| Protection | Support against flex and contact damage | Protection against abrasion, bending and mixed revisions |
| Inspection | Array-level plus position-level acceptance evidence | Individual or batch acceptance per drawing |
| Downstream equipment | SMT/test fixtures receive the joined geometry | Customer equipment accepts single boards |
On boards with precision connector fingers, shipping format influences physical damage risk. Review no-tab zones and edge protection in the hard gold finger manufacturing guide. If the order includes assembled products, coordinate the delivered state with the optical transceiver PCB assembly scope: bare-board arrays and assembled arrays can use different acceptance and handling rules.
Receiving Checks: Count, Label and Verify
A receiving clerk should not have to reverse engineer the array from a photo. The packing list should identify customer purchase order, part/revision, array drawing/revision, physical array count, accepted circuits, quantity per carton and lot identifiers where required. If the customer accepts arrays with marked rejects, the packing record must show the actual acceptable-piece count and the corresponding map or marking convention.
Five receiving checks that catch expensive mistakes
- Revision: Compare PCB and panel drawing revisions on labels against the purchase order.
- Physical versus commercial quantity: Count arrays, but also reconcile accepted circuits and defined SETs.
- Integrity: Confirm rail, breakaway and packaging condition matches the delivery agreement.
- Reject policy: Check whether marked, missing or incomplete positions are permitted, and reconcile actual accepted counts.
- Traceability and reports: Verify required lot IDs, electrical-test records, dimensional reports or other shipment documentation are present.
For mixed kits, perform these checks by distinct part number before recording complete SET quantity. An unlabeled carton containing 60 B arrays and 80 A arrays is not itself a verified delivery of 480 complete kits unless the acceptable counts and revisions agree.
Purchase Order Language You Can Adapt
The following are model clauses for purchasing communication. They are examples to adapt, not a substitute for your technical drawings, quality agreement or legal contract.
Example 1 — complete PCB array delivery
Order line: 1,200 accepted PCB pieces, part OM-101 Rev D, supplied in 100 complete 4 × 3 assembly arrays to drawing PNL-101 Rev B. All 12 shipped circuit positions in each array must meet the approved bare-board acceptance specification. Supplier may not substitute an array layout, ship rejected positions or over/under deliver without written purchaser approval. State physical array count and accepted-piece count on each packing list.
Example 2 — defined mixed-PCB SET
Order line: 480 SET. Each SET consists of 2 accepted PCB-A Rev C and 1 accepted PCB-B Rev D. PCB-A to be supplied in 12-up arrays per PNL-A Rev E and PCB-B in 8-up arrays per PNL-B Rev A, unless an alternative delivery state is authorized. Packing list must report accepted pieces by part number, physical array counts and complete-SET equivalent quantity.
Example 3 — quantity exception handling
If an ordered accepted-piece quantity is not an integer multiple of the approved all-good array, obtain written purchaser approval for the chosen overage, shortage or mixed single-piece shipment before production release.
Documents to Attach Before Order Release
Provide the latest single-board manufacturing data, part number and revision; customer-approved array drawing; total accepted piece quantity or explicit SET composition; delivery state and packaging requirements; policy for partial arrays/rejected positions; labels and inspection records; authorized over/under quantity tolerance; and the person responsible for resolving changes. Suppliers should then state whether they quote per accepted piece, per accepted array or per defined kit.
This is especially important where an unusually small board needs a special small-PCB panelization arrangement or where a contact-sensitive optical module requires edge protection. The final price should reflect the delivered unit the buyer can actually use—not an unqualified “cost per panel.”
Clarify PCB Delivery Units Before Ordering Define PCS, array configuration, acceptable good positions and shipment format in one RFQ.
PCB SET Delivery FAQs
Is one PCB SET always one panel?
No. SET is a commercial definition. It may refer to an array of identical circuits or a kit containing different designs. The buyer must state the contents.
Can I order 1,000 pieces in an all-good 12-up panel?
Only if an approved quantity exception or mixed delivery scheme resolves the integer-multiple problem. Complete arrays contain 996 or 1,008 pieces at the nearest counts.
Do panel rails count as PCB pieces?
Not in an ordinary good-circuit count. Rails, process coupons and tooling features are not functional delivered circuits unless a purchase agreement expressly defines them as products.
Can a panel containing a failed circuit count as one accepted 12-up panel?
Only if the specific PO allows it, and then the accepted-circuit count must follow the stated rule. A bad position should never be silently booked as an accepted piece.
Request a PCB Quote with Clear Delivery Units
When requesting a PCB quotation, provide the single-circuit data, array drawing, definition of PCS or SET, good-piece quantity and delivery policy. Highleap can then price a defined product instead of guessing what “500 SET” means.

Recommended Posts
Optical Transceiver PCB Manufacturer for Custom Pluggable Modules
Highleap Electronics manufactures and assembles custom...
Optical Module PCB Manufacturer for 400G, 800G and 1.6T Programs
Highleap Electronics provides optical module PCB...
Optical Communication PCB Manufacturer for Fiber Network Equipment
Highleap Electronics manufactures and assembles optical...
Optical Transceiver PCB Manufacturing in China
Highleap Electronics provides optical transceiver PCB...
How to get a quote for PCBs
Let‘s run DFM/DFA analysis for you and get back to you with a report. You can upload your files securely through our website. We require the following information in order to give you a quote:
-
- Gerber, ODB++, or .pcb, spec.
- BOM list if you require assembly
- Quantity
- Turn time
In addition to PCB manufacturing, we offer a comprehensive range of electronic services, including PCB design, PCBA, and turnkey solutions. Whether you need help with prototyping, design verification, component sourcing, or mass production, we provide end-to-end support to ensure your project’s success.
For PCBA services, please provide your BOM (Bill of Materials) and any specific assembly instructions. We also offer DFM/DFA analysis to optimize your designs for manufacturability and assembly, ensuring a smooth production process.